


In the world of industrial mining, fuel keeps all processes moving. Fuel availability directly dictates daily tonnage output. Mining operations require high-flow diesel systems for heavy-duty fuel transfer. They require a heavy duty fuel dispenser to rapidly refuel large machinery, such as haul trucks, loaders, and excavators.
Lost revenue occurs whenever large machinery idles at a fuel station. To maintain peak operational efficiency, selecting a high-flow fuel dispenser is quantifiably necessary. This ensures the system matches the throughput requirements of a 300-ton haul truck. The fuel dispenser must be capable of rapid, reliable delivery even in extreme environmental conditions.
In the world of industrial mining, fuel keeps all processes moving.’
Discover the top 10 leading manufacturers of high flow fuel dispensers for mining operations, including Aocheng Group and others. You will also learn about technical specifications that will help you choose reliable fuel dispensers.

A fuel dispenser is a heavy-duty dispensing unit designed to refuel large mining vehicles.
These units can be mounted on trucks or placed in remote locations.
A mining fuel dispenser can pump fuel very slowly (12 GPM) or incredibly fast – up to 317 gallons every single minute. It could fill a standard car’s gas tank in about 3 seconds at a very high speed.
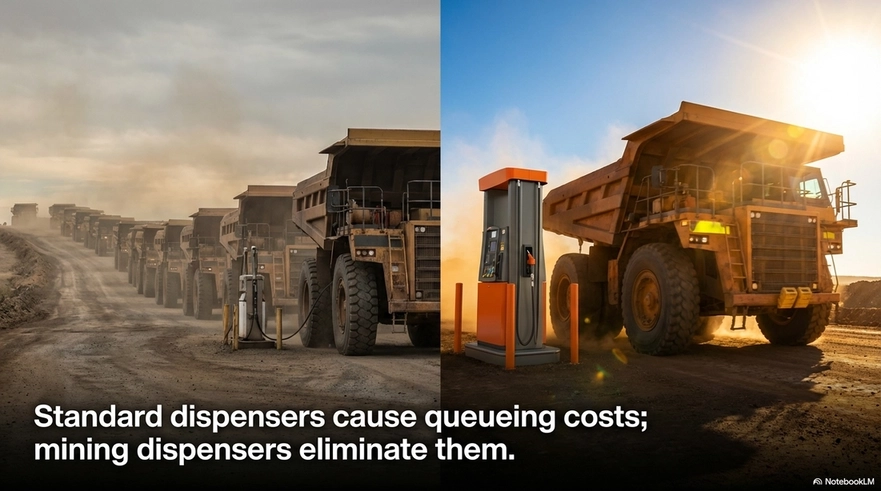
A heavy-duty fuel dispenser has great advantages in mining operations:
Inefficient refueling directly increases mining downtime costs through three critical operational challenges. When fueling systems fail to match the scale of heavy machinery, the resulting “throughput gap” leads to significant revenue loss.
A heavy-duty fuel dispenser requires a flow rate of 120L/min or more to ensure rapid refueling and eliminate operational bottlenecks. For mining and bulk transfers, this specification often extends to 200L/min+ to minimize downtime for large fleets.
To maintain this consistent high-pressure flow, the pump type must precisely match the specific tank depth and layout. Depending on your site requirements, selecting between a submersible pump or a suction-type system is critical for achieving these high-flow benchmarks.
| Feature | Mining Requirement | Why It Matters |
| Flow Rate | 120L/min to 200L/min | Reduces refueling time by up to 70%. |
| Accuracy | ±0.2% Error Margin | Vital for internal fuel accounting and loss prevention. |
| Construction | Heavy-gauge C5-M coated steel (e.g., Q235B or 304 Stainless) | Prevents corrosion and structural failure in pit sites. |
| Filtration | 10-micron particulate/water | Protects sensitive fuel injectors in modern engines. |
This technical comparison evaluates the industry’s top 10 high-flow fuel dispenser manufacturers, focusing on their distinct advantages in flow capacity, metering precision, and structural durability. By examining flagship models from leaders like Aocheng, Gilbarco, and Wayne, this analysis highlights the critical engineering differences required for demanding mining and industrial environments.
The following data provides a direct performance breakdown to help you match hardware capabilities with your specific operational volume and regulatory needs:
| Manufacturer | Flagship Model | Max Flow Rate | Key Technical Highlight (E-E-A-T) |
| Aocheng Group | AC-1200 Series | 1,200 LPM (317 GPM) | Mining Specialist: C5-M anti-corrosion; ISO 18/16/13 filtration for Tier 4 engines. |
| Fill-Rite | NX3200 Series | 95 LPM (25 GPM) | Duty Cycle: Continuous-duty motor engineered for 50°C pit environments. |
| GPI | M-3025 Series | 114 LPM (30 GPM) | Durability: Heavy-duty rotary vane design for high-viscosity diesel transfer. |
| Piusi | Bipump / ST 200 | 200 LPM (53 GPM) | Precision: Integrated bypass valves with ±0.5% electronic meter accuracy. |
| Wayne (Dover) | Select™ Series | 130 LPM (34 GPM) | Connectivity: Intelligent IoT integration for real-time remote site telemetry. |
| Gilbarco | Frontier Series | 120 LPM (32 GPM) | Compliance: High-pressure vapor recovery and Veeder-Root leak detection. |
| Petrotec | Euro-Modular | 140 LPM (37 GPM) | Chassis: 304-grade stainless steel frame resistant to abrasive iron ore dust. |
| Bennett Pump | Big-Flow Units | 150 LPM (40 GPM) | Reliability: Simple mechanical pipework for remote sites with low technical support. |
| Tokheim | Quantium™ | 130 LPM (34 GPM) | Security: Encrypted pulser systems to prevent fuel theft in unmonitored sectors. |
| Tuthill | Bulk Transfer | 570+ LPM (150+ GPM) | Volume: Specifically designed for storage bladder-to-tanker bulk movement. |
For mining operations in Australia, Indonesia, and Southeast Asia, logistics are as critical as the hardware. Aocheng Group’s strategic Thailand Hub offers significant shipping advantages.

In summary, selecting the right high-flow fuel dispenser is paramount for optimizing mining productivity and ensuring operational efficiency in the evolving 2026 landscape. Balancing ultra-high flow rates, structural durability, and manufacturer transparency is the most reliable way to future-proof your fueling infrastructure and eliminate costly bottlenecks.
As a specialist in heavy-duty energy solutions, Aocheng Group delivers the certified performance and engineering precision required to meet these demanding global benchmarks. We hope these insights help you choose a solution that not only ensures site safety but also supports your long-term growth.


 10월 30,2026


